Applications of Pneumatic Conveying
Cement plants for efficient powder and fly ash conveying, improving plant productivity.
Food processing industries for hygienic and safe material transfer, ensuring product quality.
Pharmaceutical plants for precise and controlled powder handling, meeting industry standards.
Chemical and plastic industries for bulk material movement, enhancing production capacity.
Mineral processing plants for dust-free conveying systems, maintaining a clean work environment.
Manufacturing units requiring automated material handling to optimize processes and reduce manual labor.
Uses of Pneumatic Conveying System
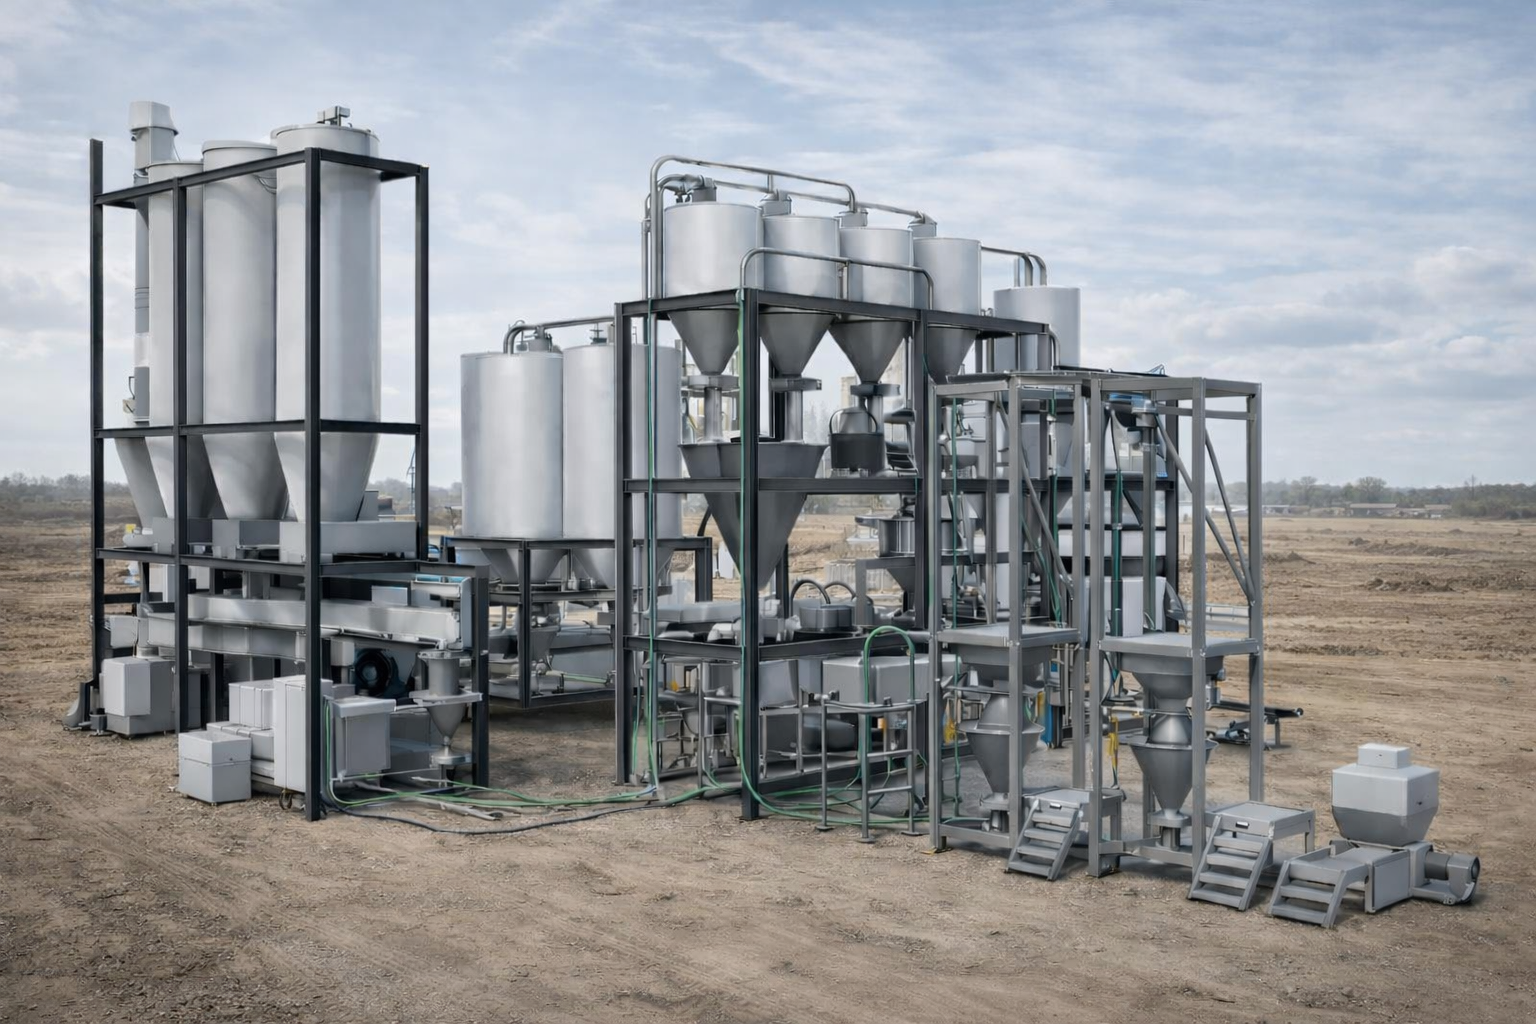
Dust-free transportation of bulk materials through pipelines for enhanced workplace safety.
Efficient handling of powders, granules, and pellets, ensuring smooth material flow.
Automated material transfer with minimal human intervention, increasing operational efficiency.
Reduced material loss and contamination during conveying, ensuring product integrity.
Consistent material flow and process optimization, contributing to continuous production.
Improved plant cleanliness and operational safety, reducing environmental and safety hazards.